
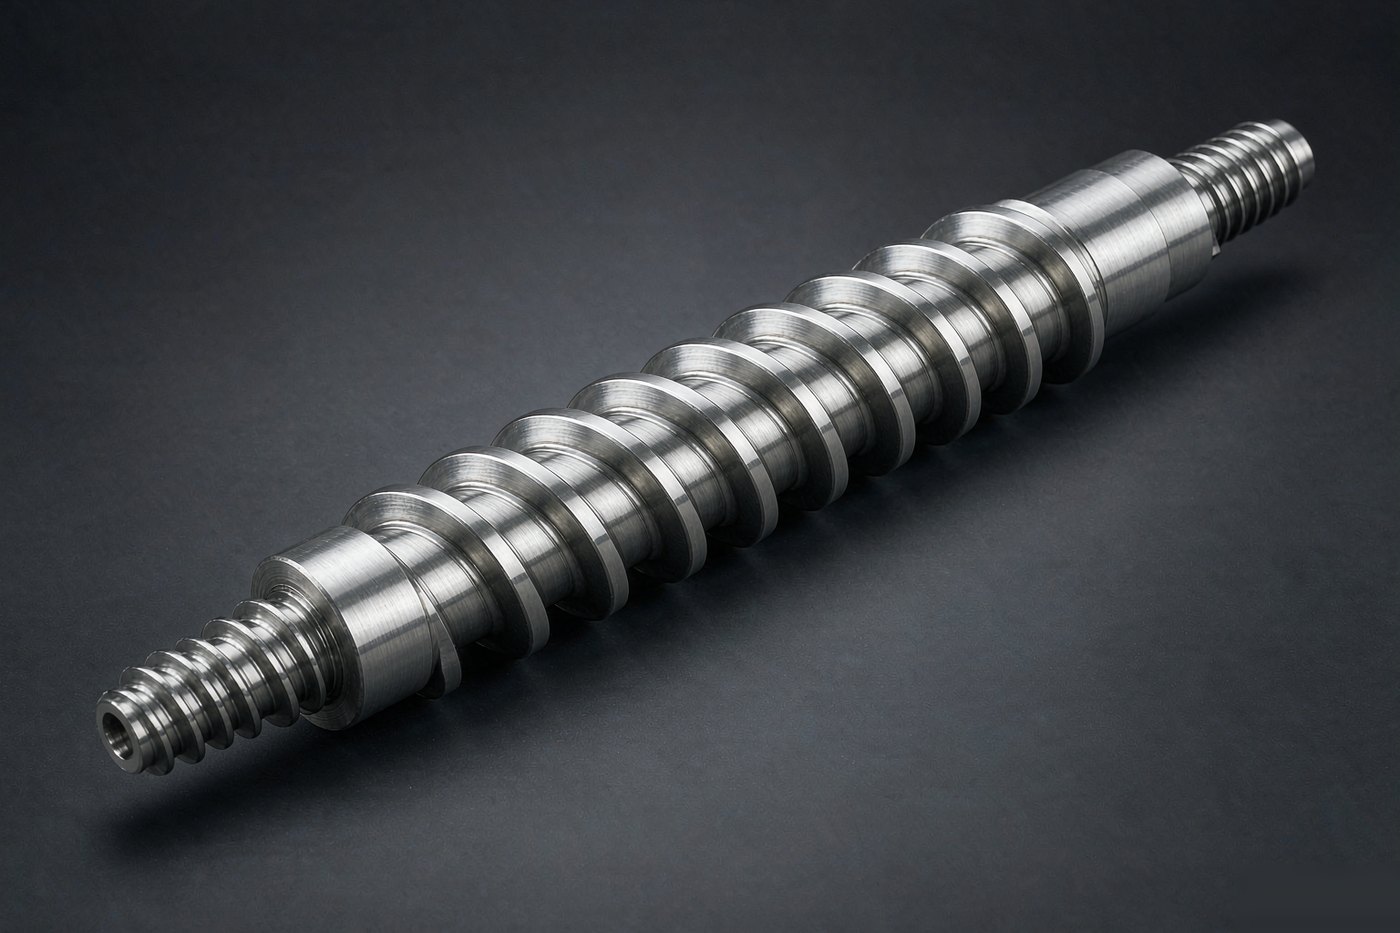
General Purpose Screw for PP, PE and ABS
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
View details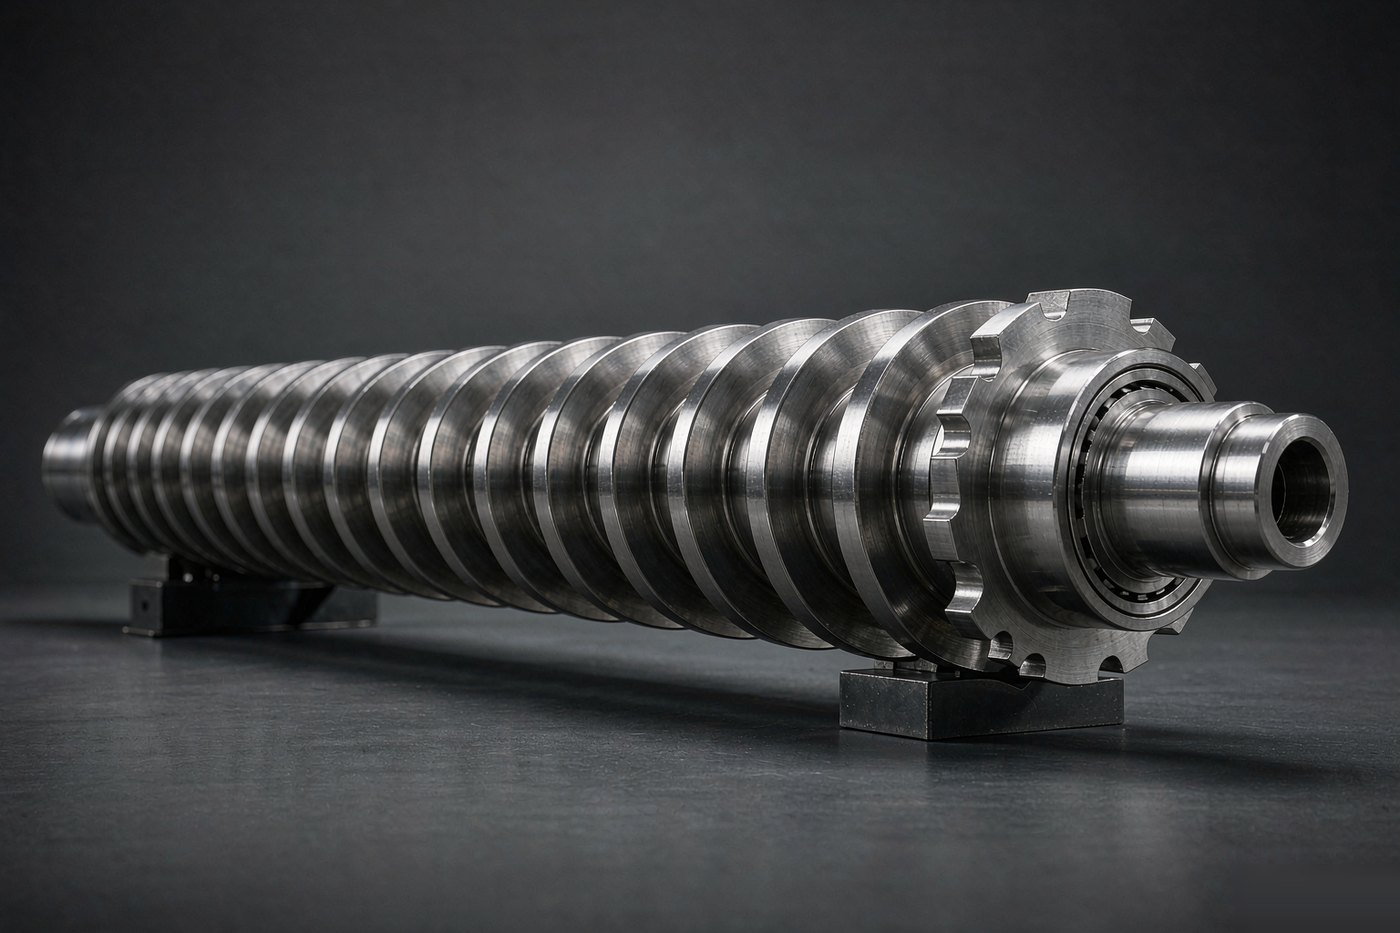
Separates solids from melt for a more even melt temperature on large shots and narrow processing windows.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
A barrier screw separates what a general purpose screw cannot: it keeps solid resin and already melted polymer apart along the whole melting length. A secondary flight runs beside the main flight, the solid bed is trapped in the channel it leaves, and melt that forms is forced over the barrier into the metering channel.
The result is a melt that is fully plasticized at a lower average temperature, because the solid is not being dragged through a melt pool that is already hot.
| Parameter | Typical range | Note |
|---|---|---|
| Screw diameter | Matched to your barrel bore | Barrier screws are cut per order, not stocked |
| L/D ratio | From about 24:1 upward, depending on output target | Longer screws give the barrier zone room to work |
| Barrier flight clearance | A few hundredths of a millimeter over the main flight | Too much and the solid bed leaks past; too little and it scores the barrel |
| Barrier flight lead | Set against the main flight pitch | Controls how fast the melt is drawn off the solid bed |
| Compression ratio | Often lower than a general purpose screw | The barrier does the work; excessive compression adds shear heat |
We size the barrier zone against your output target and resin, and confirm the profile on a drawing before cutting.
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
View details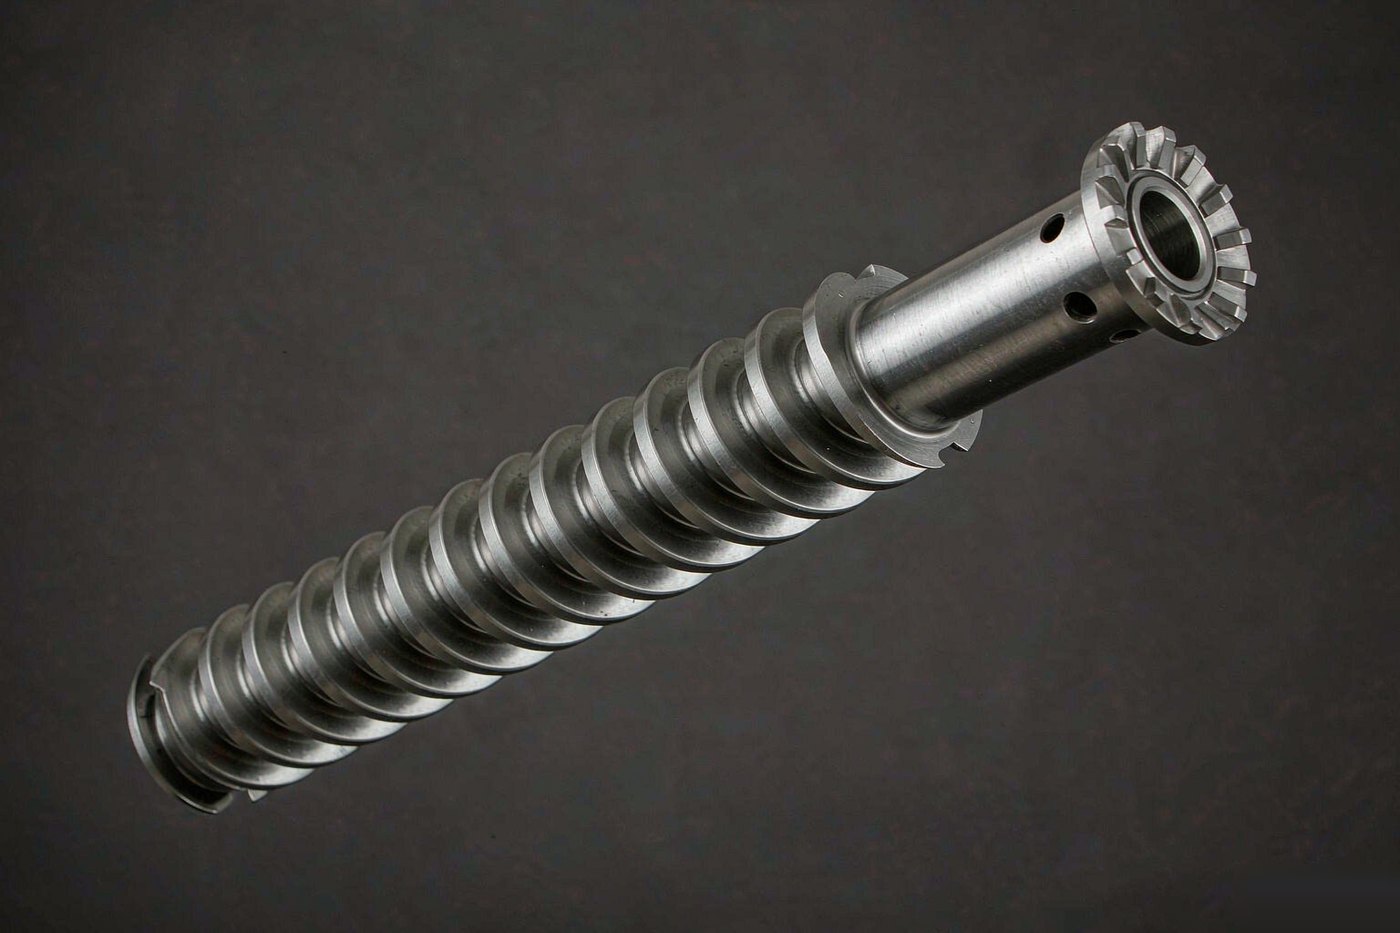
Adds a dispersive or distributive section to solve color streaks, specks and temperature variation.
View details
Separates solids from melt for a more even melt temperature on large shots and narrow processing windows.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.