
 01
Screws for injection molding
Flight depth, pitch and compression matched to the resin you run and the shot weight you need.
View screwsCentron machines the wear parts at the heart of your injection molding process — screws, barrels, tip assemblies and nozzle bodies — matched to your press, your resin and your cycle.
Every part we make sits in the same flow — from the feed throat to the gate. We build them as a set so the geometry works together instead of fighting itself.
01
Flight depth, pitch and compression matched to the resin you run and the shot weight you need.
View screws 02
Bores and feed zones aligned to the screw they have to work with — not bought in as a separate item.
View barrels 03
Tips, rings and seals that hold the shot under pressure and survive the wear at the front end.
View assemblies 04
The last hundred millimeters of the melt path, where surface finish and temperature decide part quality.
View nozzlesA screw that is hard but badly matched to the resin wears out just as fast as a soft one. We start from what the material does to the steel.
Alloy grade and surface treatment are chosen against the abrasion and corrosion profile of the resin — glass-filled, corrosive or commodity — rather than taken from a catalogue default.
Turning, milling and grinding to the tolerances a screw needs to run true inside its barrel, with the flight profile cut to the specification agreed on the drawing.
Bore, outer diameter, runout and surface condition are checked against the drawing before a component is packed for shipment.
Most premature screw failures are not material failures. They are geometry decisions that were never matched to the process — too much shear, too little compression, a mixing section that does not disperse the color.
 Illustrative view
Glass- and mineral-filled grades wear flights fast. Alloy and surface treatment follow the filler load.
Long runs on commodity resin: stable output and quick, clean color changes matter more than peak speed.
Thin-wall, high-cavitation tools need fast plasticizing and a shot weight that repeats cycle after cycle.
Small shots, tight tolerance. Melt temperature has to hold steady from the nozzle to the gate.
Fine detail and short cycles put the emphasis on melt homogeneity and nozzle temperature control.
Abrasive PVC and filled compounds: corrosion protection and liner hardness decide service life.
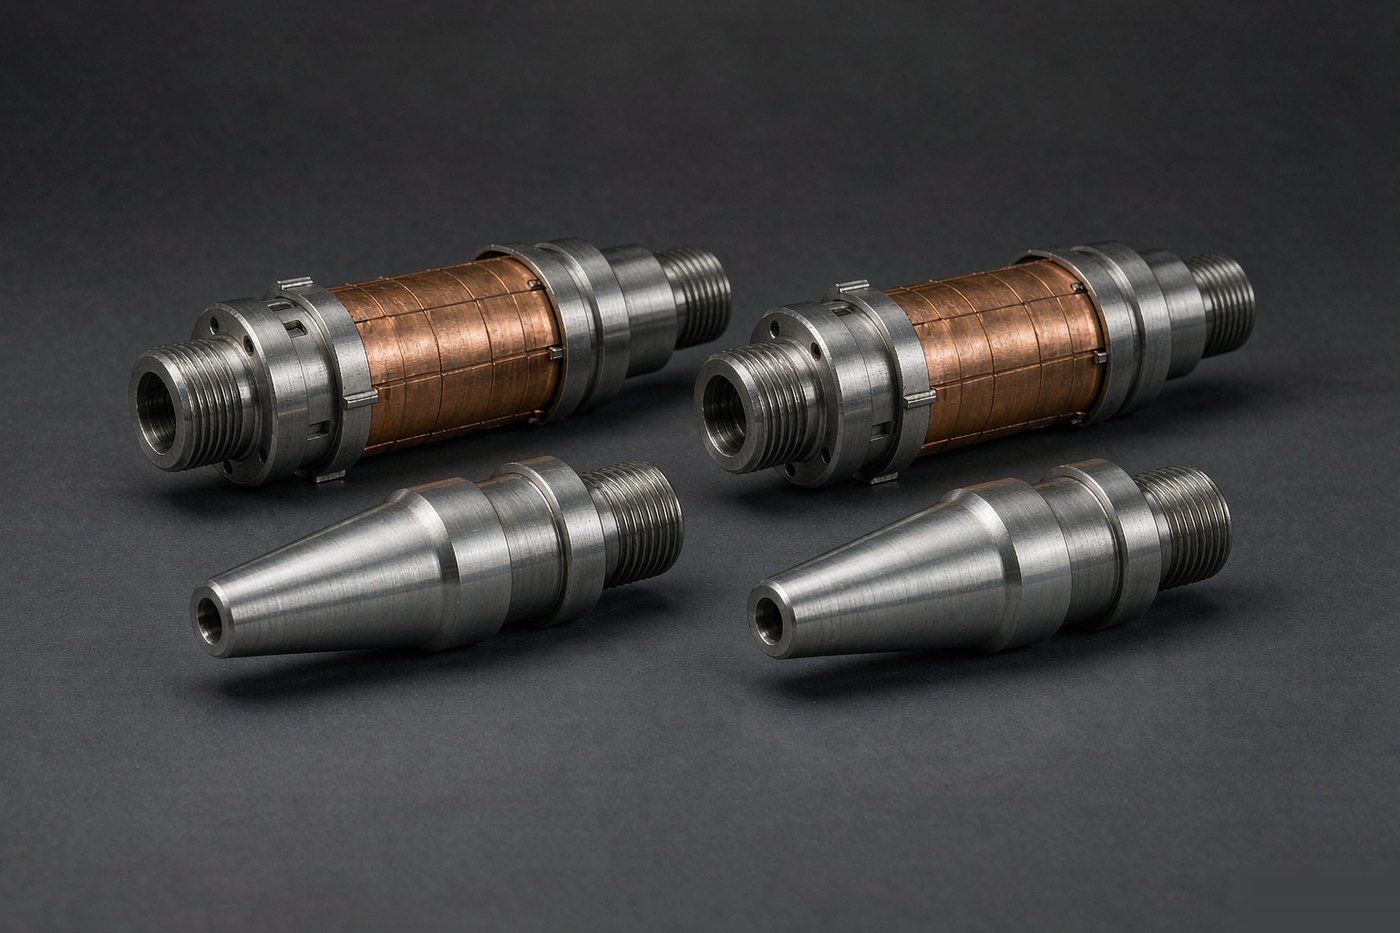
The order flow behind every Centron screw and barrel: written specification before quotation, machining stages, per-drawing inspection and the records shipped with the batch.
Read more
Base steels behind injection screws and how to choose between nitriding, hard chrome, bimetallic overlay and tungsten carbide by resin and filler.
Read more
Four process signs of check-ring failure - drifting cushion, part weight spread, rising shot demand and unstable packing - plus what to inspect at teardown.
Read moreTell us the press, the screw diameter, the L/D ratio and what you run. You get a dimensional proposal and a price — not a catalogue page.