
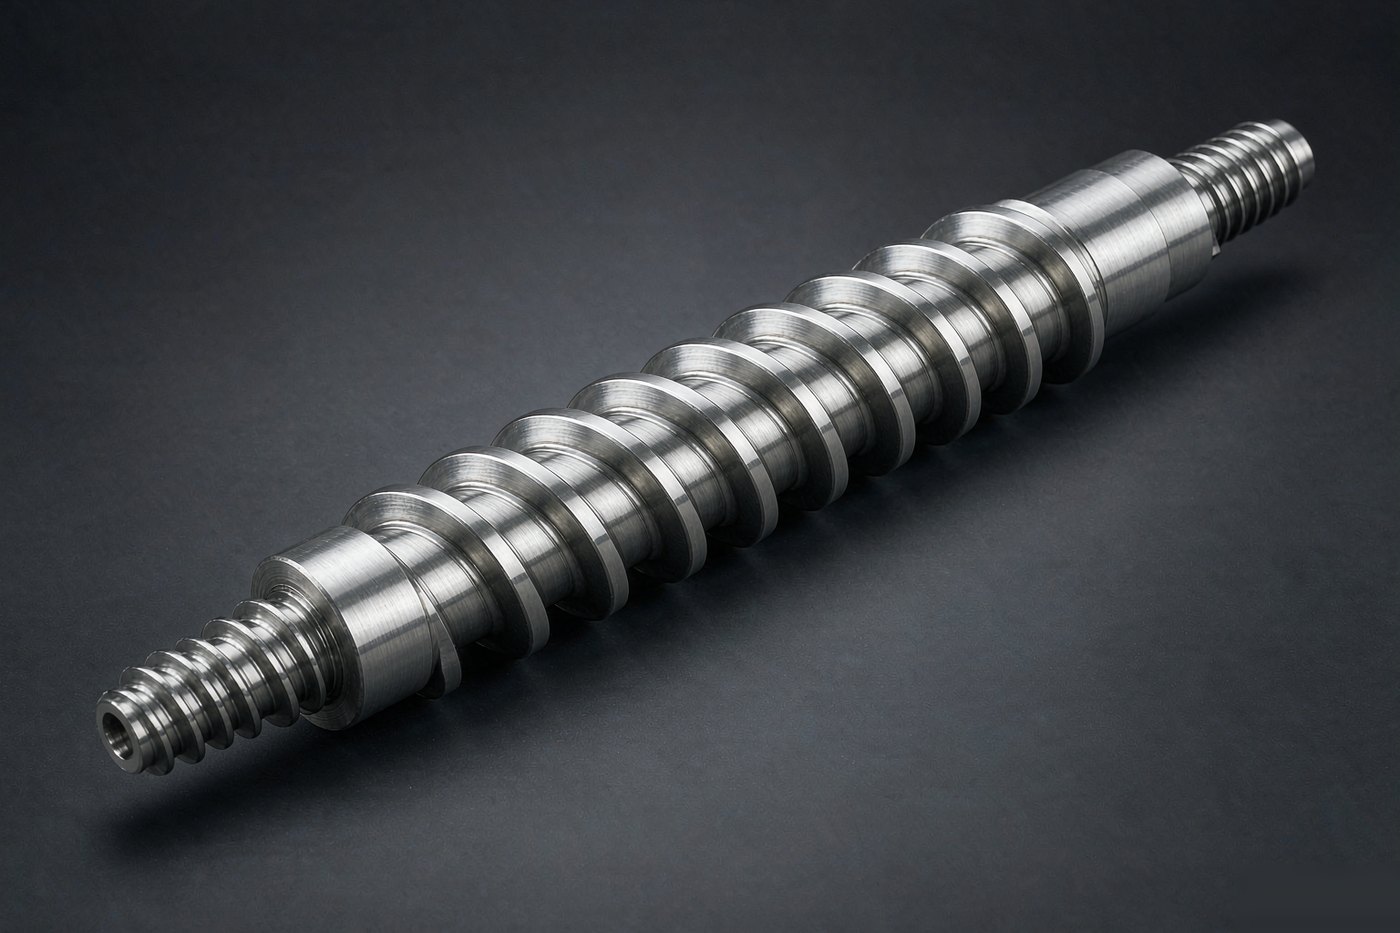
General Purpose Screw for PP, PE and ABS
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
View details
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
A general purpose screw is the conventional three-zone design: feed, compression and metering on a single flight. It is the right choice for commodity resins — PP, PE, PS, ABS and their blends — where the priority is steady output rather than fine dispersion.
| Parameter | Typical range | How it is set |
|---|---|---|
| Screw diameter | Matched to the barrel bore you are running | Measured from your drawing or the worn screw |
| L/D ratio | Usually 20:1 to 25:1 for injection molding | Longer L/D gives more melting length; the machine barrel limits the maximum |
| Compression ratio | About 2.0 to 3.0 for commodity polyolefins | Raised for crystalline resins, lowered for heat-sensitive ones |
| Feed depth | Deep channel, roughly 0.12 to 0.18 times diameter | Set so the solids can be conveyed without bridging |
| Metering depth | Feed depth divided by the compression ratio | Shallow enough to build pressure, deep enough not to shear-burn |
| Flight pitch | Usually around one diameter | Changed when the resin needs a different conveying angle |
Parts that do not demand tight color control, thin-wall filling or high shear mixing. If your rejects come from unmelt, color streaks or unmixed masterbatch, a general purpose screw is usually the wrong tool — a barrier or mixing design will fix it more cheaply than process tuning ever will.
We cut the flight geometry to suit those inputs and confirm the drawing before machining starts.
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
View details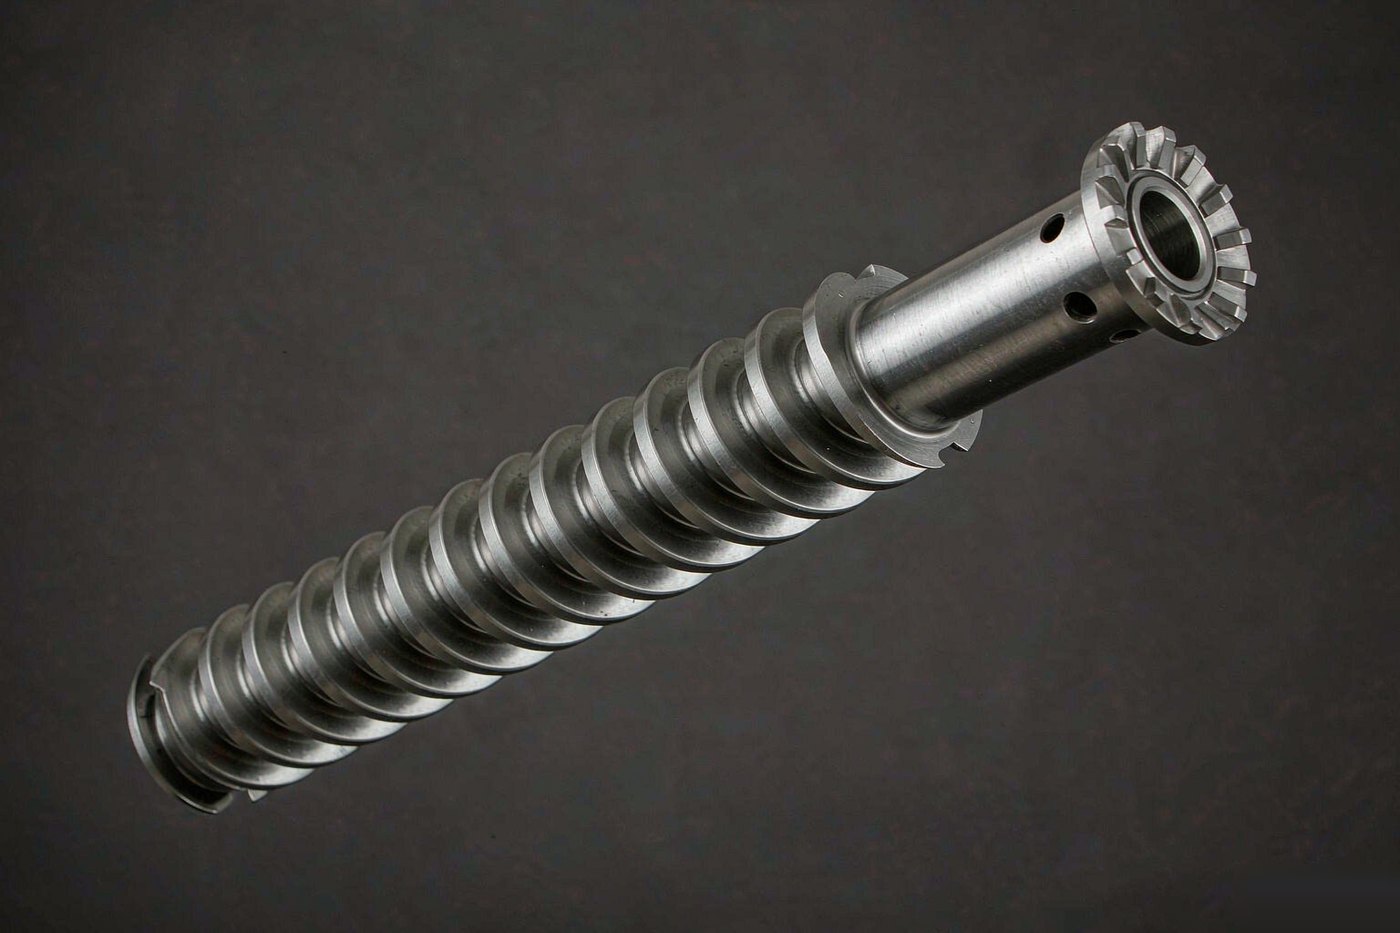
Adds a dispersive or distributive section to solve color streaks, specks and temperature variation.
View details
Injection and extrusion screws in nitrided, bimetallic and hard-chrome finishes, cut to your barrel dimensions and screw geometry rather than to a catalogue number.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.