

Nozzle Tips — Matched to Resin and Gate
Sets the orifice that decides shear, drool and stringing at the gate.
View details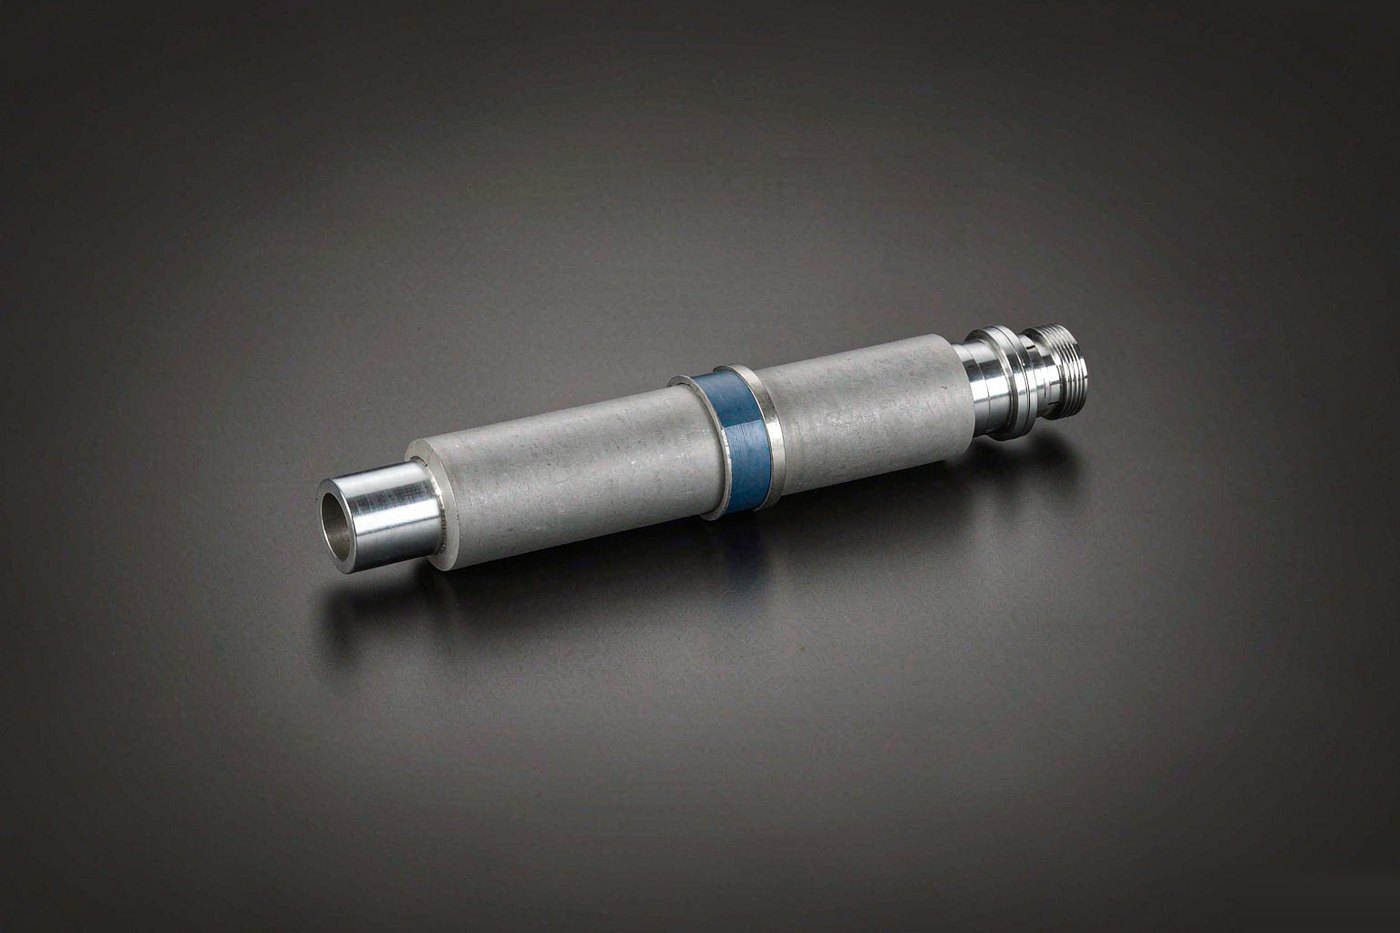
Reaches the sprue when the standard nozzle cannot; heated or unheated.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
An extension adds length between the nozzle body and the tip. It is the part you fit when the barrel cannot reach the sprue bushing, or when a deep mold needs the melt delivered further forward.
| Parameter | Typical range | Note |
|---|---|---|
| Length | From a few millimeters to several hundred | Set by the measured gap, not estimated |
| Heater | Usually required above about 60 mm | An unheated extension acts as a cold slug trap |
| Internal bore | Matched to the body bore, no step | A step creates a dead zone that degrades resin |
| Thread and seat | Same forms as the body it screws into | Confirmed against the body drawing |
| Straightness | Critical on long extensions | Runout shows up as seat leakage |
Sets the orifice that decides shear, drool and stringing at the gate.
View details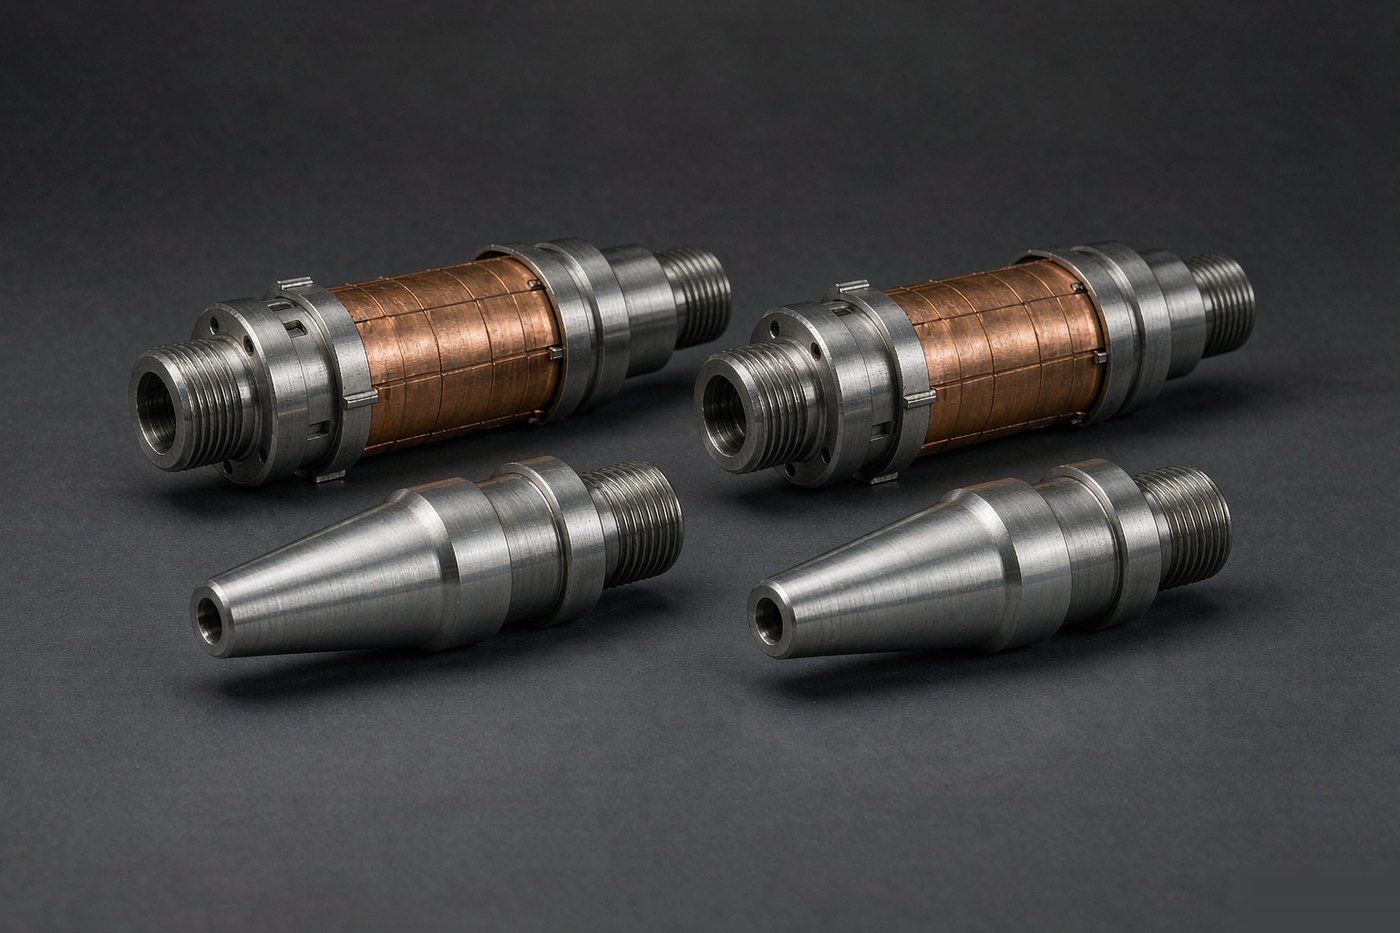
Final section of the melt path, carrying the heater band up to the sprue.
View details
Reaches the sprue when the standard nozzle cannot; heated or unheated.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.