
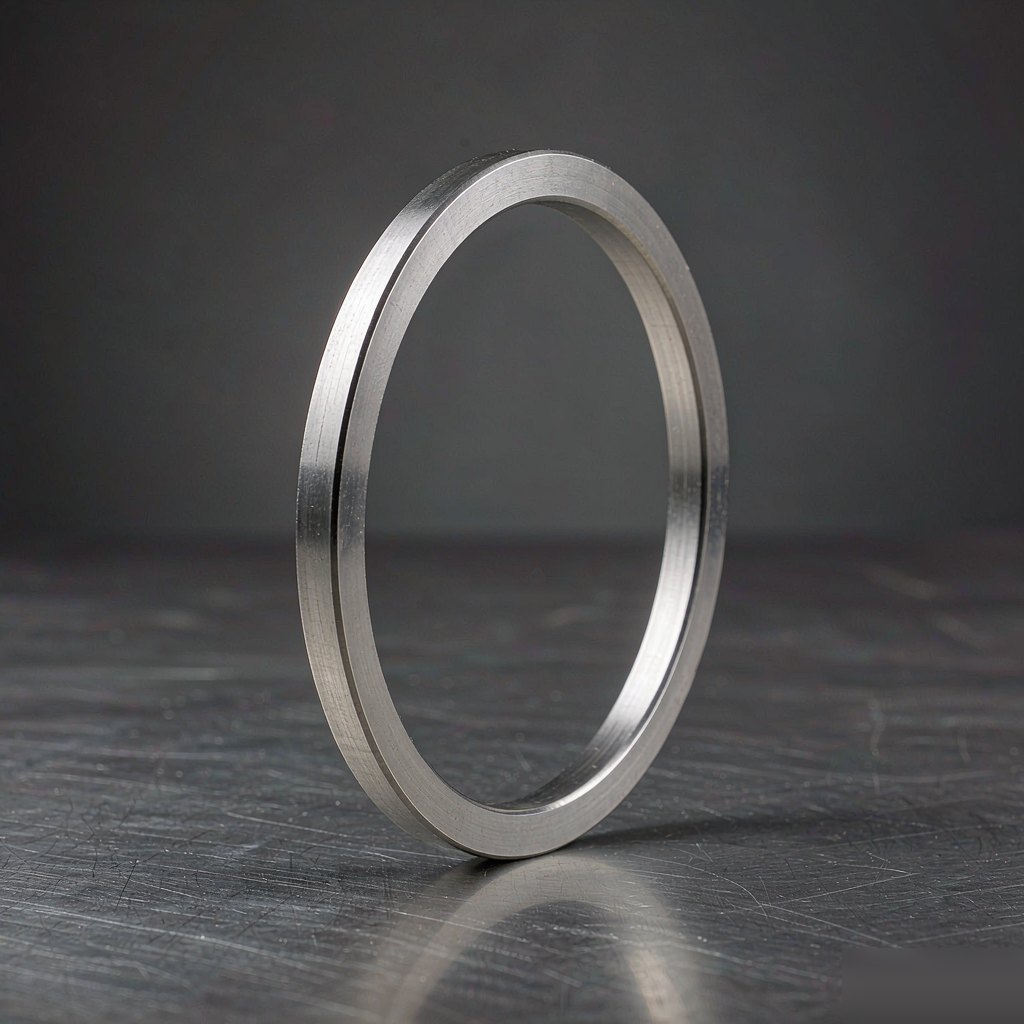
Seal Ring - Keeping Melt Out of the Drive End
Limits leakage past the tip; matched to the wear profile of the assembly.
View details
Screw tip assemblies for injection units: tips, non-return rings, seats and seal rings, matched to the screw end and the resin.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
The screw tip is a small part with a large job: it has to seal against back-flow during injection, then open cleanly during recovery. When it stops sealing, the symptom is a cushion that will not hold and parts that vary in weight from shot to shot.
Tips are matched to the screw end and to the resin. A free-flow tip is fine for a commodity grade and wrong for a low-viscosity engineering resin that will run past it.
| Type | How it seals | Use it for |
|---|---|---|
| Free-flow | No check element; relies on melt viscosity and screw geometry | Commodity PE, PP, PS where a small back-flow is tolerable |
| Non-return ring | A sliding ring seats against a shoulder on the forward stroke | The general-purpose choice for engineering resins; simple and repairable |
| Ball check | A ball seats in a conical seat | Low-viscosity resins that would slip past a ring; needs a clean melt |
| Sliding ring, heavy duty | Ring with a hardened seat and a longer guide | Filled and abrasive compounds, high back-pressure settings |
Tip dimensions are matched to the screw end you send or draw. The type selection above is the starting point for that conversation, not a stock list.
Limits leakage past the tip; matched to the wear profile of the assembly.
View details
Screw tip assemblies for injection units: tips, non-return rings, seats and seal rings, matched to the screw end and the resin.
View details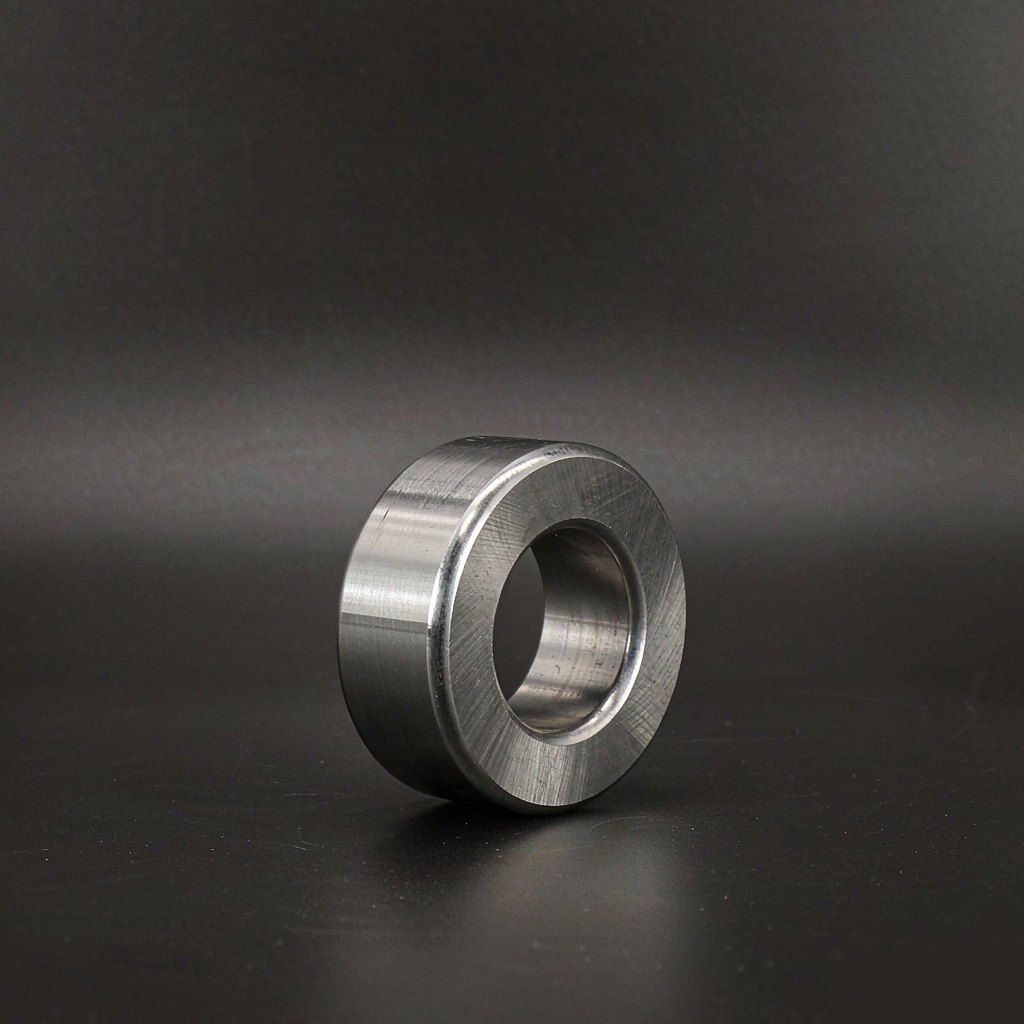
Prevents melt flowing back over the screw and keeps shot weight consistent.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.